Batch Traceability in Food and Feed Plants With SAP Business One
 Asem Alkamel
11 min read
In this article
- What batch traceability has to deliver
- Where traceability breaks in feed and food plants
- Setting up SAP Business One for batch traceability
- Which items to manage by batch
- Batch control at every transaction or on release only
- Batch attributes
- A batch numbering scheme
- The traceability chain from receipt to dispatch
- Where the MES fits: actuals instead of theory
- Running a recall drill
- Mistakes that quietly break traceability
- Key takeaways
- Frequently asked questions
- What is the difference between batch traceability and lot traceability?
- Does SAP Business One support batch traceability?
- How do you trace a batch backward to its raw materials?
- How fast should a product recall trace be?
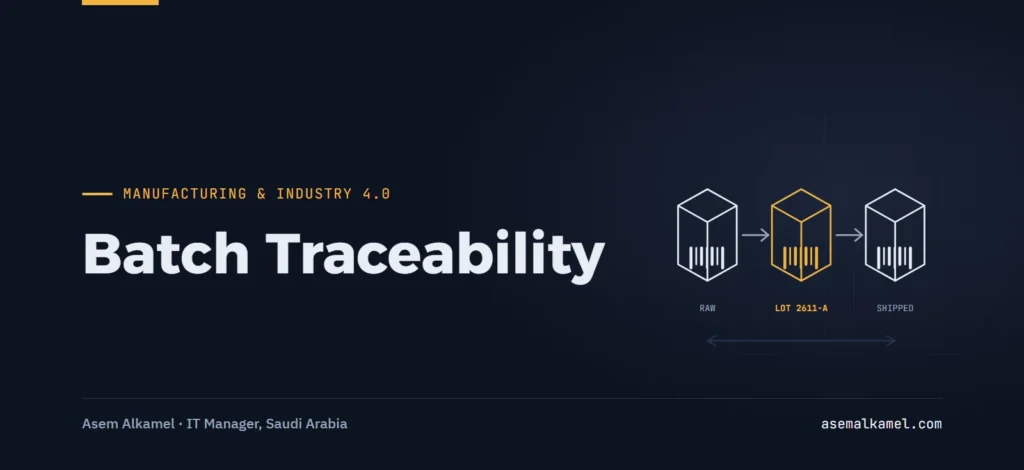
Batch traceability means being able to answer two questions quickly and with evidence: which raw material lots went into a given finished batch (backward trace), and which finished batches and customers received a given raw material lot (forward trace). In a food or feed plant running SAP Business One, you get there by managing the right items by batch, assigning batch numbers at receipt and at production, and making sure actual consumption, not the theoretical recipe, is what gets recorded.
I manage IT at NAF Company, a feed manufacturer in Al-Qassim, where SAP Business One is integrated with an MES and a custom feed formulation system. Before that integration, the link between a bag of finished feed and the lots of raw material inside it lived in production sheets that someone later reconciled by hand. Now batch actuals from the floor reach the ERP in real time, and the reconciliation job is gone. The notes below are what I would tell a plant manager or an ERP project owner who is about to set this up.
What batch traceability has to deliver
Regulators, customers’ auditors and your own quality team all ask the same two things, in opposite directions:
- Backward trace (one step back): finished batch FG-2026-0417 contains which lots of corn, soybean meal, premix and additives, received from which suppliers on which dates?
- Forward trace (one step forward): premix lot PX-7731 was consumed in which production batches, and those batches were delivered to which customers on which invoices?
The test is whether you can answer in minutes, from the system, with a document trail an auditor accepts. If a recall requires a meeting, it is not traceability; it is archaeology.
Where traceability breaks in feed and food plants
Process plants have features that make lot traceability harder than in discrete manufacturing, and they are where I have seen records fall apart:
- Bulk storage. Grain goes into a silo that already contains the previous lot. There is no clean one-lot-per-bin unless you enforce it operationally.
- Formulation changes. The recipe for the same product changes with ingredient prices and nutrition targets. If the ERP’s bill of materials lags the formulation system, the “theoretical” consumption used for backflushing is wrong.
- Rework and returns. Off-spec product reintroduced into a later batch carries its own ancestry; if it is booked as a generic ingredient, the chain breaks.
- Manual dosing of micro-ingredients. Hand-added premixes and additives are the most likely to be consumed without a lot being recorded.
- Timing. Production is recorded at the end of the shift from paper; by then, which lot was open at the time of the batch is a guess.
Each of these is a process decision first and a system setting second.
Setting up SAP Business One for batch traceability
SAP Business One supports managing items by batch numbers, and the official documentation on managing batch numbers in SAP Business One describes the basics. The decisions that matter at setup time:
Which items to manage by batch
All raw materials that end up in product, all intermediates, all finished goods, and packaging in direct contact with the product. Consumables and spare parts should not be batch-managed; it adds data entry without traceability value.
Batch control at every transaction or on release only
SAP Business One lets you require a batch number on every transaction (receipts and issues), or only on release (issues). For traceability, choose every transaction for product-touching items: a lot that enters without a number cannot be traced out. “On release only” is a convenience for items where inbound lot identity does not matter, and that is rarely true for ingredients.
Decide this before go-live. Changing the batch management setting on an item that already has stock is disruptive, so set it right in the item master during implementation rather than retrofitting it. The ERP data migration checklist covers loading opening stock with batch numbers, which is the other half of the same decision.
Batch attributes
Each batch carries quantities per warehouse and properties such as expiration date. Decide what populates the dates: the supplier’s certificate for raw materials, production date plus shelf life for finished goods. A batch with no expiration date will never trigger a first-expired-first-out pick.
A batch numbering scheme
Numbering is a policy, not a system feature. The scheme below is an example: unique, sortable, human-readable, and distinct from supplier lots.
Raw material receipt batch:
  RM-<ITEMCODE>-<YYYYMMDD>-<GRPO no.>-<seq>
  e.g. RM-CORN01-20261019-10457-01
  Supplier lot number stored as a batch attribute, never as the key.

Production (finished goods) batch:
  FG-<LINE>-<YYMMDD>-<shift>-<seq>
  e.g. FG-L2-261019-A-07

Rework / returned goods:
  RW-<original FG batch>-<seq>
  e.g. RW-FG-L2-261019-A-07-01
Two rules: never use a supplier’s lot number as your batch key (two suppliers can use the same string), and never let rework lose the batch it came from.
The traceability chain from receipt to dispatch
A batch number must be captured at each of these steps; miss one and both traces break there.
- Goods receipt. Each delivery line creates one or more receipt batches; the supplier’s lot and certificate reference are recorded as attributes. Bulk deliveries into a shared silo are received as their own batch even if the silo mixes them physically; the trace will then show every lot that could be in the silo during a window, which is the honest answer.
- Transfer to production stores or bins. Stock transfers carry the batch; the system now knows which lots are at which line.
- Formula release. The formulation system produces the recipe version; the ERP bill of materials and the MES recipe are updated from it, not edited by hand. Record the recipe version on the production order.
- Dosing and consumption. The MES records actual quantities per ingredient and the lot each was drawn from, including hand-added micro-ingredients. This is the step where “theoretical” consumption is replaced by actual consumption.
- Receipt from production. The finished batch is created with its FG batch number, production date and expiration date, and the ERP posts the consumption and receipt from the MES data.
- Quality release. The batch stays on hold or in a quarantine warehouse until released; the release decision is recorded against the batch.
- Delivery and invoice. Delivery notes carry the batch numbers shipped, so forward trace reaches the customer.
| Step | Document in SAP Business One | Batch created or consumed | Usual failure |
|---|---|---|---|
| Goods receipt | Goods receipt PO | Created (RM) | Supplier lot used as key; no expiration date |
| Transfer | Inventory transfer | Carried | Transfer posted after use, wrong lot picked |
| Consumption | Issue for production (from MES actuals) | Consumed (RM) | Backflushed from BOM, not actuals; micro-ingredients skipped |
| Output | Receipt from production | Created (FG) | Output booked once per shift, not per batch |
| Release | Transfer from quarantine / status change | Carried | Released stock shipped before the decision is recorded |
| Dispatch | Delivery, A/R invoice | Shipped (FG) | Batch not selected at delivery; picked FIFO on paper |
Where the MES fits: actuals instead of theory
An ERP on its own consumes what the bill of materials says, when someone posts the document. That backflushing is fine for traceability only if actual consumption always matches the recipe and the open lot is always the one the ERP assumed. In a feed plant, neither holds.
The MES closes that gap. It knows the batch that ran, the scale readings per ingredient and the lot each hopper was loaded from. When those actuals post to SAP Business One as the issue for production and the receipt from production, the batch genealogy in the ERP is a record of what happened, not an estimate. Which system owns which data is the subject of MES vs ERP on the factory floor; the short version for traceability is that the MES owns actual consumption and the ERP owns the inventory and the documents.
This is also where acceptance testing earns its keep. When I audited our delivered MES against the signed requirements with a 60-point test plan over four cycles, we found 3 defects and about 20 functional gaps, and that evidence supported a controlled partial acceptance rather than a sign-off. If traceability is a requirement, put explicit scenarios for lot capture and actuals posting in your user acceptance testing.
Running a recall drill
A recall drill is the only honest test of batch traceability. Run one before an auditor or a customer makes you. The procedure:
- Pick a raw material lot at random from receipts of the last 60 days, preferably a micro-ingredient, because that is where recording is weakest.
- Start the clock. Note the time the quality manager receives the “contaminated lot” notice.
- Forward trace in the ERP. Use the batch transactions report in SAP Business One to list every production batch that consumed the lot, then every delivery and invoice that shipped those batches. Record the customer list and quantities.
- Backward trace one finished batch. For one of the affected FG batches, list every ingredient lot and supplier. Compare against the MES record for the same batch.
- Reconcile quantities. Received minus consumed minus on hand should be zero for the raw material lot; produced minus shipped minus on hand should be zero for each FG batch. Any gap is a hole in the chain.
- Stop the clock and write the gaps. Every manual step, every spreadsheet consulted and every call to the floor becomes an action item.
- Repeat quarterly and track the time to a complete answer.
A reasonable target for a mid-sized plant with an integrated ERP and MES: a full forward and backward trace with reconciled quantities in under two hours, by one person. If the first drill takes a day, that is the number you will improve.
Mistakes that quietly break traceability
- Batch-managing finished goods but not raw materials. You can tell the customer what batch they got and nothing about what is in it.
- Letting the ERP backflush while an MES exists. Two records of consumption, one estimated and one measured, and the estimated one ends up in the ledger.
- Recipe versions edited directly in the ERP. The formulation system is the owner; manual edits create a BOM nobody can match to a formula.
- Rework booked as a generic item. Its ancestry disappears.
- Delivery notes without batch selection. The warehouse picks one lot and the document shows another.
- Reporting from the screen. A recall needs a query, not scrolling. I build production and quality reports in SAP Business One as SQL queries and Crystal Reports so that the trace is a report, not a search.
Key takeaways
- Batch traceability is two queries, forward and backward, that must be answerable in minutes from the system with a document trail.
- In SAP Business One, manage every product-touching item by batch, require batch numbers on every transaction, and set this before go-live.
- Use your own batch keys; store supplier lot numbers as attributes, and keep rework linked to its original batch.
- Actual consumption recorded by the MES, not theoretical backflushing, is what makes the genealogy true in a process plant.
- The chain has seven capture points from receipt to dispatch; a missed step breaks both traces at that point.
- Run a recall drill quarterly, time it, reconcile quantities, and turn every manual step into an action item.
Frequently asked questions
What is the difference between batch traceability and lot traceability?
In practice they are the same discipline. “Lot” is more common for raw materials received from suppliers, and “batch” for what a plant produces in one run. SAP Business One uses the term batch numbers for both. What matters is that each quantity of material, received or produced, carries an identifier that follows it through every transaction.
Does SAP Business One support batch traceability?
Yes. Items can be managed by batch numbers, with batch numbers required on every transaction or on release only, and batches carry properties such as expiration date. The batch transactions report shows the movement history of batch-managed items, which supports forward and backward tracing. For actual consumption at the dosing level, most process plants pair it with an MES.
How do you trace a batch backward to its raw materials?
Start from the finished batch number, open its receipt from production, and read the linked issue for production to list every ingredient batch consumed. Each ingredient batch then points back to its goods receipt, supplier and certificate reference. This only works if consumption was posted with the actual lots used, which is why MES actuals matter more than the bill of materials.
How fast should a product recall trace be?
With an integrated ERP and MES and disciplined batch capture, a mid-sized plant should complete a full forward and backward trace with reconciled quantities in under two hours, by one person, from the system. Plants relying on paper and spreadsheets typically need a day or more and still cannot reconcile quantities precisely. Regular drills are how you move from the second number to the first.
If you are implementing SAP Business One in a food or feed plant, or you have it running and a recall drill would worry you, I can help you design the batch setup, the MES integration and the traceability reports from the company’s side. See the ERP implementation service, the feed manufacturing case study, or contact me directly.